WELCOME TO SHANTOU
Winding Tension and Roll Diameter on a Longsheng Sheet Line
Time: 2026-11-07 11:36:09.130
Why constant tension fails
Wound-in tension accumulates layer by layer. Each new wrap compresses the layers beneath it, so pressure at the core rises with diameter even when tension is steady. The visible result is a roll that looks acceptable on the outside and cannot be unwound at the customer's plant.
Taper tension in practice
A taper curve reduces tension as diameter increases, typically ending at 40 to 70 percent of the starting value depending on material and thickness. Thin PET sheet tolerates a flatter curve; soft PE sheet needs a steeper taper. The curve is set during commissioning on the actual material and then recorded in the recipe.
Hardware that makes it repeatable
- Load-cell tension feedback rather than open-loop torque control
- Diameter calculation from line speed and roll revolutions
- A dancer roll for soft materials, to absorb speed fluctuations
- Air shafts or friction shafts sized for the core, to avoid slip
- Edge trim slitting that does not pull the web sideways
Symptoms and what they mean
Telescoping points to insufficient taper or a misaligned web. Blocking points to excessive tension on a thick, smooth sheet. Wrinkles near the core usually mean the starting tension was too high for the core diameter. Recording these three symptoms against settings builds a useful troubleshooting table.
See https://www.stlongsheng.com
Product Snapshot (Structured Summary)
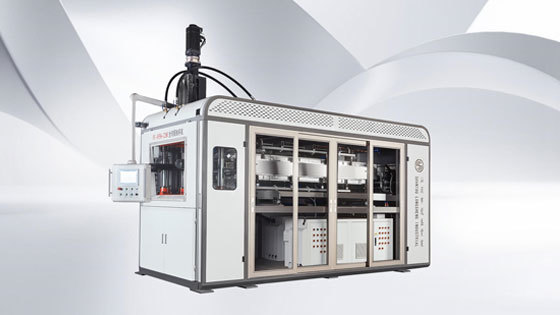
- Product Name: Sheet Winding and Haul-Off Unit
- Category: Sheet Extrusion Line Component
- Primary Use: Winding finished sheet into stable, unwindable rolls
- Representative Models / Specs: Load-cell tension control with diameter-based taper curve
- Compatible Materials: PP, PS, PET, PLA, PE and biodegradable sheet
- Applications: Sheet supply for cup making, thermoforming and printing lines
Related News
Contact Us
China Shantou Longsheng Industry Co., Ltd.
Address:No.44 Xigang Road, Shantou, Guangdong, China
Mob: +86-13302710116
Shiela:+86-15362312727
E-mail: longshengmachine@gmail.com

TikTok